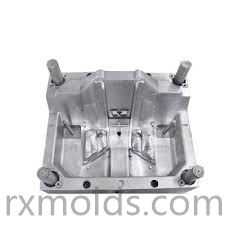
The increasing use of engineered plastics has changed how many vehicle components are designed and manufactured. Modern production combines material science, precision tooling, process control, and inspection to create components with integrated functions and complex geometry. Within this environment, Injection Molding Car Parts provides a practical manufacturing method for producing repeatable plastic components across different automotive applications.
Automotive plastic parts can serve structural, functional, protective, decorative, or assembly-related purposes. Interior trim, housings, brackets, covers, bezels, ducts, and lighting components may all require different combinations of strength, dimensional stability, appearance, and thermal resistance. These requirements influence material selection as well as mold construction and injection process planning.
Material behavior should be considered before the tooling design is finalized. Different engineering polymers exhibit different flow characteristics, shrinkage rates, thermal responses, and mechanical properties. A material with good impact resistance may behave differently during filling and cooling from one selected for high-temperature stability or surface appearance. Understanding these characteristics helps engineers develop suitable gates, runners, cooling systems, and cavity structures.
Product geometry is another major consideration. Modern vehicle components may include thin walls, deep sections, ribs, bosses, mounting points, clips, and curved surfaces. These features can affect filling and create challenges during demolding. Design-for-manufacturing analysis allows engineers to review wall thickness, draft angles, parting lines, undercuts, and other details before mold construction begins.
Mold flow simulation can support this analysis by providing a digital representation of material movement through the cavity. Engineers can evaluate filling balance, pressure distribution, weld-line locations, potential air entrapment, and other conditions. The information can then be used to review gate locations, runner design, venting, and processing strategies before the physical tooling is manufactured.
Cooling design has a direct relationship with dimensional stability. After molten polymer enters the cavity, heat must be removed in a controlled manner before the component can be released. Areas with different wall thicknesses may cool at different rates, potentially contributing to deformation or dimensional variation. Cooling channels should therefore be planned according to the actual geometry rather than relying on a uniform arrangement.
Temperature control during production is equally important. Changes in material temperature, mold temperature, or cooling conditions can influence viscosity, filling behavior, shrinkage, and surface appearance. Stable process control helps reduce unnecessary variation between production cycles. Monitoring key production conditions can also make it easier to identify the source of defects when they occur.
Ejection requires careful engineering because molded automotive parts may contain delicate edges, deep cavities, or visible surfaces. Ejector pins, sleeves, lifters, and other mechanisms should be positioned according to the structural characteristics of the component. Adequate draft angles can reduce resistance during release, while balanced ejection forces can help minimize deformation and unwanted marks.
Cavity surface quality also affects the final appearance of visible parts. Depending on the application, a mold may require polished surfaces, controlled textures, or other specialized finishes. These surfaces must be prepared consistently so that the intended appearance is reproduced throughout production. Precision grinding and polishing may be required after primary machining to achieve the specified cavity condition.
Machining accuracy forms the physical foundation of the tooling. CNC machining can create complex three-dimensional cavity and core structures, while EDM can produce fine features and geometries that are difficult to machine conventionally. Inspection during these stages helps confirm that the manufactured tooling remains consistent with approved digital data.
Trial production is used to verify the interaction between mold design, material, and processing conditions. Engineers can inspect sample parts for dimensions, surface appearance, filling, ejection, and assembly compatibility. If a deviation is found, the cause should be evaluated systematically rather than assuming that the mold itself is always responsible. Material conditions and processing parameters can also influence the final result.
Automation can further support production consistency. Automated material handling, robotic part removal, visual inspection, and production monitoring can reduce manual variation in repetitive operations. For automotive programs involving sustained production, these systems can also support traceability and more structured quality management.
Maintenance should be considered throughout the mold lifecycle. Repeated production exposes moving components, cavity surfaces, cooling passages, and alignment features to mechanical and thermal conditions. Regular inspection and appropriate maintenance can help identify wear before it affects molded parts and can support more stable long-term tooling operation.
The overall manufacturing process is most effective when product design, simulation, tooling, machining, molding, and inspection are treated as connected stages. Taizhou Renxin Mould Co., Ltd. integrates mold engineering, simulation, precision machining, finishing, and production validation, with further information available at https://www.rxmolds.com for manufacturers developing precision solutions for Injection Molding Car Parts and other automotive plastic components.